Set takt from the erection plan, balance block stages against it and feed the line with drawingless, model-based work packages, with a worked example.
In a shipyard, lean and digital tools solve two halves of the same problem. Lean gives you a disciplined, standardized flow of work. Digital tools show whether that flow is holding and get the right information to the person doing the work. Layered on an unstandardized process, they mostly produce a faster view of the same waste.
This article stays practical: setting takt from the erection plan, balancing block stages against it with a worked example, sizing buffers, modeling a takt line in a scheduling tool, and what a drawingless, model-based work package must contain for the line to hold its rhythm.
Lean Principles, Adapted to a One-Off Product
Lean was built for repetitive, high-volume manufacturing, and a ship is neither. What survives is the logic, not the literal tools. Value is defined from the owner's side: on-time delivery, zero defects at sea, lifecycle cost, class compliance. The value stream is mapped at several levels (project, grand block, panel line, outfitting cell) because one end-to-end map is too coarse to act on. Work is pulled by the erection schedule rather than pushed ahead of need.
It works despite low-volume, high-mix production because a vessel is still built from many repeated interim products: panels, standard brackets, pipe spools, outfitting units. The ship is unique; most of its parts are not, and standardizing at that level is where most of the real gain comes from. Research from the University of Rijeka on converting a traditional panel-block assembly process to one-piece flow makes a related point, pairing lean with group technology and a product work breakdown structure (Kolić, Fafandjel and Zamarin, Brodogradnja, 2012).
Value Stream Mapping: Where the Waiting Actually Is
A current-state map of a typical block, from steel arrival through cutting, forming, welding, NDT and outfitting, tends to show that the dominant waste is not the work but the waiting between steps: a panel parked because the next station is occupied, a block waiting for NDT sign-off before it can move to outfitting.
To make the map useful, walk one real block through the process and record two numbers per step: time being worked on and time sitting. Mark where material is pushed regardless of readiness. The map also gives you the stage list and work content for the takt calculation.
Setting Takt Time from the Erection Plan
The Lean Enterprise Institute defines takt time as available production time divided by customer demand (LEI Lexicon: takt time). The "customer" of a block line is the berth or dock, so takt is set from the erection plan, not from what the shops currently manage.
A worked example (illustrative, hypothetical figures). A single-shift yard must deliver one grand block every two working days to the slipway. Productive time per shift, after breaks, safety briefings and planned stops, is 380 minutes. Two working days of one shift each give 760 minutes of available time per block: that is the takt, about 12 hours 40 minutes. Every upstream process (panel line, sub-assembly, block assembly, outfitting, blast and paint) has to be balanced against it. A process that structurally cannot keep pace is where the schedule will break, however good the plan looks on paper.
Takt is not cycle time. Cycle time is what a process actually takes, measured on the floor (LEI Lexicon: cycle time); takt is what the erection plan demands. Planning is closing the gap.
Balancing the Stages Against Takt: A Worked Example
For each stage, divide one grand block's worth of work content (man-hours) by the crew. That gives the hours the block occupies the station. Compare it with the available time: takt multiplied by the number of parallel stations. Treating a grand block's worth of panels as one unit is a simplification, but the arithmetic is the same.
| Stage | Man-hours | Crew | Hours per block | Load before | Change | Load after |
|---|---|---|---|---|---|---|
| Panel line | 135 | 12 | 11.2 | 89% | none | 89% |
| Sub-assembly | 200 | 18 | 11.1 | 88% | none | 88% |
| Block assembly | 600 | 20 | 30.0 | 237% | 3 parallel bays, plus 80 man-hours of outfitting | 89% |
| Block outfitting | 260 | 16 | 16.2 | 128% | 80 man-hours moved to block assembly | 89% |
| Blast and paint | 3 shifts of cell time | n/a | 19.0 | 150% | second cell | 75% |
| Grand block joining | 160 | 15 | 10.7 | 84% | none | 84% |
All figures hypothetical, for illustration only.
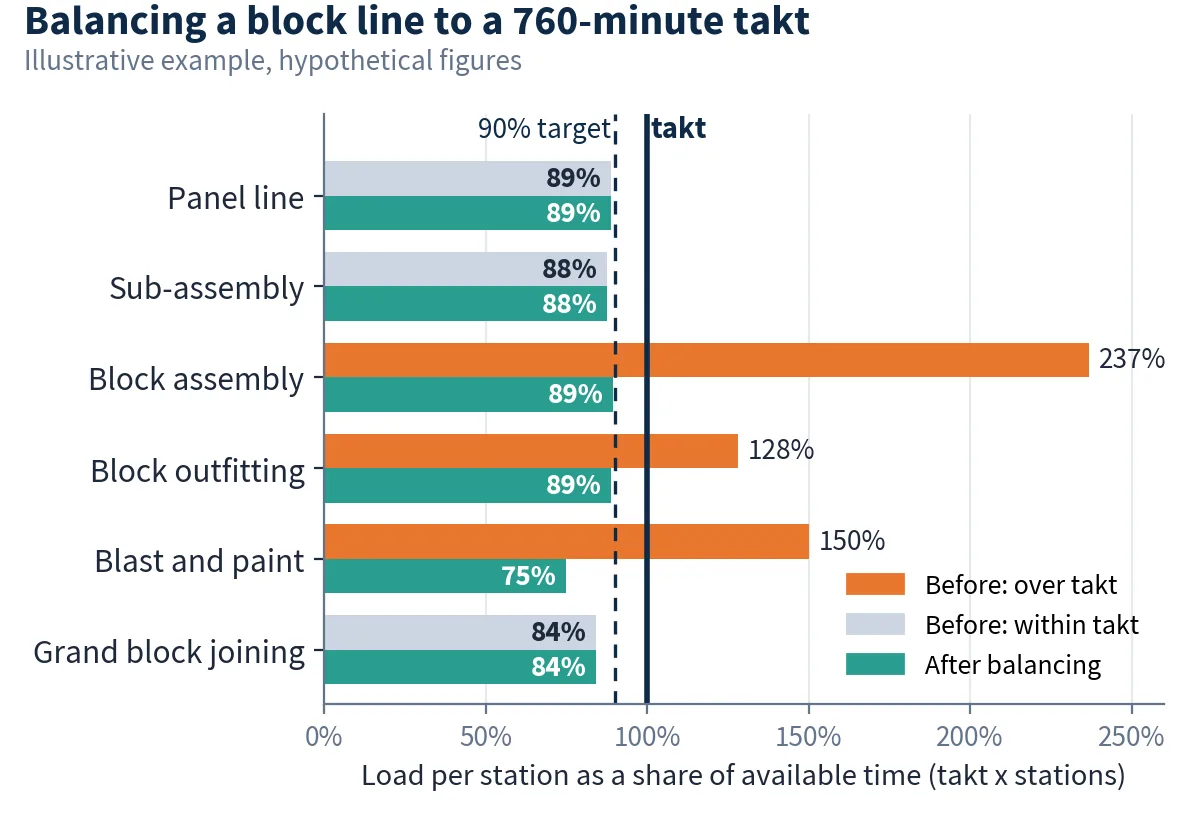
Three stages fail, and each needs a different fix:
- Block assembly at 237% is a work-content problem that overtime will not solve. With three parallel bays, a new block enters every takt and each bay has three takts (about 38 productive hours) per block.
- Block outfitting at 128% is fixed by moving work, not adding people. The assembly bays now have slack, so 80 man-hours of pipe, foundation and cable-tray work move there, while the block is open and access is easier: the logic of pre-outfitting at block stage. Pushed into sub-assembly instead, the same hours would take that stage well over takt. Moving work only helps if it lands where there is slack.
- Blast and paint at 150% is a cell-occupancy problem: blasting, coating and cure hold the cell whatever the crew size. A second cell or a faster-curing coating system is the real answer. The block construction schedule article explains why this stage is so often underestimated.
Total work content stayed at 1,355 man-hours; only where, and in how many parallel places, it happens changed. The chart uses a 90% target because a station loaded exactly to takt has no room for a late plate or a repair. The LEI describes the aim as loading each operator to "very nearly equal to, but slightly less than, takt time" (LEI Lexicon: operator balance chart). The margin itself is a yard decision.
Blocks Are Not Identical
Real blocks differ: an engine room block carries far more outfitting than a parallel midbody block. Group blocks into families of similar work content and sequence erection so heavy and light blocks alternate, so each station sees an average load near takt rather than a spike. Newport News described grouping similar steel pieces into "unit families" on carrier work so lessons carry from one to the next (Defense News, March 2022). Lean construction research takt-plans non-repetitive work by zoning it and capping each step at the same fixed time, with workload per zone as the common unit (Tommelein, Journal of Construction Engineering and Management, 2022). The yard equivalent is adjusting block division so each block-stage package sits close to the takt load.
Sizing Buffers with Little's Law
Little's Law says average work in process equals throughput multiplied by average flow time, L = λW (Little, Operations Research, 2011). In the balanced example there are nine station slots (four single stations, three assembly bays, two paint cells), so a block spends nine takts, or 18 working days, in the line. At half a block per working day, work in process is 0.5 × 18 = 9 grand blocks' worth. Add two finished blocks buffered in front of the berth and the yard needs laydown space and transport for eleven.
In reverse: if waiting stretches flow time to 30 working days, work in process grows to fifteen at the same output. A storage area that fills while erection output stays flat means waiting is rising somewhere.
Putting a Takt Line into MS Project
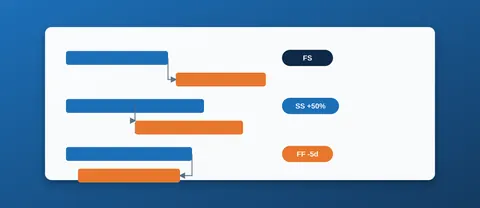
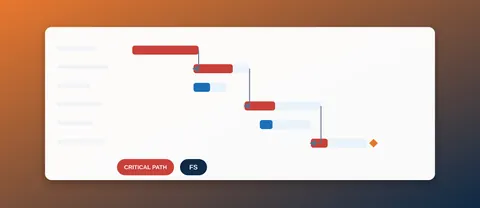
A takt line needs two kinds of finish-to-start link:
- Product flow: each stage of block n follows the previous stage of the same block.
- Station occupancy: each stage of block n follows the same stage of block n minus k, where k is the number of parallel stations. With three bays, assembly of block 7 follows assembly of block 4.
Durations are multiples of takt (two working days here). The task dependencies lesson covers link types and lags. Alternatively, model each bay or paint cell as a capacity-limited resource and let leveling resolve occupancy, as in resource leveling and crane/dock capacity planning. Explicit links are easier to review; leveling is easier to change when the bay count changes.
Running to Takt: The Daily Check
A takt plan means little unless the shop measures against it. The simplest form is a board with one row per station and one column per takt: did the block leave when due? Every "no" gets one reason code from a short, fixed list:
- material or kit incomplete
- model or work package not released, or changed after release
- crane or transporter not available
- quality hold (NDT, dimensional check, class or owner inspection)
- crew shortfall
- rework from upstream
After a few weeks the codes show whether the problem is capacity, which the balancing table can fix, or readiness, which it cannot. Readiness is where digital tools earn their place.
5S, Standard Work and Just-in-Time
In welding bays and pipe shops, 5S (shadow boards, color-coded material zones, andon signals for a stoppage) cuts time spent looking for tools and material. Standard work for repetitive tasks, plus accuracy control that keeps blocks within erection tolerance, reduces one of the costliest hidden losses: rework found only when a block does not fit. Just-in-time means material kitted for the takt in which it is needed, not weeks early, which only adds congestion and damage risk. Kanban pull suits brackets, consumables and pipe spools. The kit list should come from the same source as the work package, so what arrives matches what the instructions say to install.
Drawingless Production: From the 3D Model to the Work Package
"Drawingless" production means the shop builds from the 3D product model, delivered as visual work instructions on a laptop or tablet, instead of from 2D paper drawings extracted from it. A 2016 Newport News paper named "a drawingless work environment for the craftsman" as a goal of its digital shipbuilding effort (Debbink, ASNE FMMS 2016).
The change is gradual. According to Defense News, the Ford class was designed in 3D, but Ford and Kennedy were built from paper drawings derived from the model because step-by-step digital work instructions were not ready; Kennedy was used to trial them, and Enterprise (CVN 80) is being built fully with digital work instructions on laptops, including 3D views that can be rotated and enlarged (Defense News, March 2022; HII, June 2023). In commercial work, Samsung Heavy Industries announced in September 2024 a yard-wide rollout of a 3D digital production drawing system replacing paper production drawings and inspection documents (SHI announcement). In 2020 ABS reported approving Israel Shipyards' 3D models in plan review of a 45-meter patrol vessel in place of 2D class drawings (ABS news, September 2020). These are announcements and program descriptions, not measured results.
The link to takt is direct. Many "no" codes on a takt board are readiness failures: the crew reached the block and the information was unclear, outdated or missing. A model-based package does not create discipline by itself, but it removes the step where someone interprets a drawing set and the risk of a superseded revision staying on the floor. The revision control underneath is covered in document control and technical data packages.
What a Model-Based Work Package Should Contain
On paper or on a tablet, a package released to a takt station should answer every question the crew would otherwise walk to the office to ask:
- Identity: package number tied to block and stage, the model revision it was cut from, release date.
- Start and end state: the interim product as it arrives and as it must leave, not the finished ship.
- Parts and kit: part marks, quantities and kit location, matching what was delivered.
- Sequence: fit-up and welding order, with welding procedure references.
- Outfitting at this stage: every pipe piece, foundation, penetration and support fitted here, shown in place.
- Dimensional control: check points, tolerances and measurement method.
- Hold points: inspections that stop work until signed off, linked to the inspection and test plan.
- Planned effort: man-hours and crew, so the supervisor can see it was loaded to takt.
- Feedback route: how the crew reports a clash, missing part or model error, and who answers within the takt.
Two release rules keep it honest. Release only when the model area for that block is frozen and the kit is confirmed; an early package just moves the waiting from the office to the floor. And any model change after release produces a new package revision, flagged at the station.
The wider toolset fits the same frame: a digital thread keeps the bill of materials, packages and CNC programs on one model revision, and a yard simulation can test a bay allocation before the schedule is committed. None of it works on a chaotic process.
Where This Tends to Go Wrong
- Takt is set from shop capacity instead of erection demand, so the plan never exposes the stage that cannot keep up.
- Averages hide heavy blocks. A line balanced on the average block fails whenever an engine room block arrives.
- Work is moved to a stage with no slack, which only relocates the bottleneck.
- Tablets arrive before the model is mature. If model areas still change at release, a drawingless package carries the same churn as a drawing set, only faster.
- A pilot on one panel line is declared a yard-wide win before checking whether its conditions (labor, block complexity, material flow) hold elsewhere.
- Automation targets the most visible bottleneck rather than the stage actually constraining flow, and the erection date does not move.
Takt tells each station how much work it can absorb; a good work package lets the crew start the moment the block arrives. For the erection sequence that sets the takt in the first place, the block erection sequence plan template is a practical starting point.